 Skip to content

By the Arclight Dynamics team · Updated September 24, 2026 · 9 min read
Quick Answer: What Plasma Cutter Do You Need for a CNC Table?
Choose the plasma cutter by the thickest metal you cut every day, not the thickest you might cut once a year. For most shops that means a Hypertherm® Powermax45 SYNC for material up to ½", a Powermax65 or Powermax85 SYNC for ½"–¾" work, and a Powermax105 SYNC or Powermax125 when you pierce ⅞"–1" plate daily. Production shops piercing 1¼" run the MAXPRO200 on an Arc Max Unlimited, and shops that need laser-like edges run the Hypertherm XPR170 or XPR300 on the Arc Max X. Whatever the amperage, a CNC table needs a machine torch and a CPC port — and every Arclight table is quoted with the Hypertherm system matched to your work, so you are never guessing.
In This Guide
How Do You Match Plasma Cutter Amperage to a CNC Table?
Amperage decides two things on a CNC plasma table: how thick you can pierce and how fast you can cut. The number that matters for CNC work is pierce capacity — the thickest plate the system will start a hole in from the middle of a sheet, which is what happens on every nested part. Cut (severance) capacity is a bigger number, but it only applies when you start from an edge, and it is not a production rating.
Here is how the Hypertherm systems Arclight pairs with its tables stack up. The pierce and cut figures are on mild steel; the add-on price is what each system adds to a table quote in the configurator on our product pages.

| Hypertherm® system | Amperage | Pierce capacity (mild steel) | Cut capacity (mild steel) | Shop power | Add-on price on an Arclight table |
|---|---|---|---|---|---|
| Powermax45 SYNC | 45 A | ½" | 1" | Single phase | $3,710 |
| Powermax65 SYNC | 65 A | ⅝" | 1" | Single or three phase | from $4,700 |
| Powermax85 SYNC | 85 A | ¾" | 1¼" | Single or three phase | $6,550 |
| Powermax105 SYNC | 105 A | ⅞" | 1½" | Three phase only (200–600 V) | $7,750 |
| Powermax125 | 125 A | 1" | 1½" | Three phase only (480–600 V) | $11,200 |
| MAXPRO200 | 200 A | 1¼" | 2" | Three phase only (200–600 V) | $22,245 (Arc Max Unlimited) |
| XPR170 | 170 A | 1⅜" air shield / 1⁹⁄₁₆" argon-assist | 2⅜" severance | Three phase | Included with Arc Max X |
| XPR300 | 300 A | 1¾" O₂ / 2" argon-assist | 3⅛" severance | Three phase | Included with Arc Max X |
Pierce capacity is what the system will start a hole in unassisted — the number that matters for production nesting. Cut capacity is the maximum it will part from an edge. Add-on prices are the configurator prices on arclightcnc.com as of September 2026 and match Hypertherm’s published pricing; the Arc Max X is sold as a complete system with the XPR included.
The working rule: pick the system whose pierce rating covers the plate you cut every week, then go one size up if you spend real time near the top of that range. A Powermax45 SYNC will sever 1" steel from an edge, but if you nest parts out of ½" plate all day you will spend your life waiting on pierces and changing consumables — a Powermax65 or 85 pierces the same plate faster, cleaner, and with a longer consumable life. Higher amperage also means higher travel speed on thin material, which is why production shops running 16-gauge through ¼" still buy an 85 or 105: throughput, not thickness, pays for the upgrade.
Which Plasma Cutter Pairs With Each Arclight CNC Table?
Every Arclight table is engineered around Hypertherm systems, and every table product page has a configurator where you pick the cutter as line one of the quote. The options are wide on purpose — a 4×4 Arc Pro Ultra V3 can carry a Powermax125 if that is the work — but the pairings below are where most shops land, and they are the ones Arclight recommends first.
| Arclight table | Controller | Cutter options in the configurator | Most common pairing | Best for |
|---|---|---|---|---|
| Arc Pro Ultra V3 | ArcCNC | Powermax45, 65, 85, 105 SYNC, Powermax125; Razor Cut 45di entry option | Powermax45 or 65 SYNC | First tables, metal art, signage, small shops cutting up to ½" daily |
| Arc Pro Elite V3 | FlashCut CNC | Powermax45, 65, 85, 105 SYNC, Powermax125; Razor Cut 45di entry option | Powermax65 or 85 SYNC | Small shops that want FlashCut CNC end to end, up to ¾" daily |
| Arc Max Ultra | ArcCNC | Powermax45, 65, 85, 105 SYNC, Powermax125 | Powermax65 or 85 SYNC | Small fab shops stepping up to a heavier frame |
| Arc Max Elite | FlashCut CNC | Powermax45, 65, 85, 105 SYNC, Powermax125; dual-torch and HySpeed servo options | Powermax85 or 105 SYNC | Fab shops cutting plate every day, up to ⅞" pierce |
| Arc Max Unlimited | FlashCut CNC | Powermax45–125, MAXPRO200, Kjellberg K200, or provide your own | MAXPRO200 | Heavy plate and high-volume production, 1¼" pierce / 2" cut |
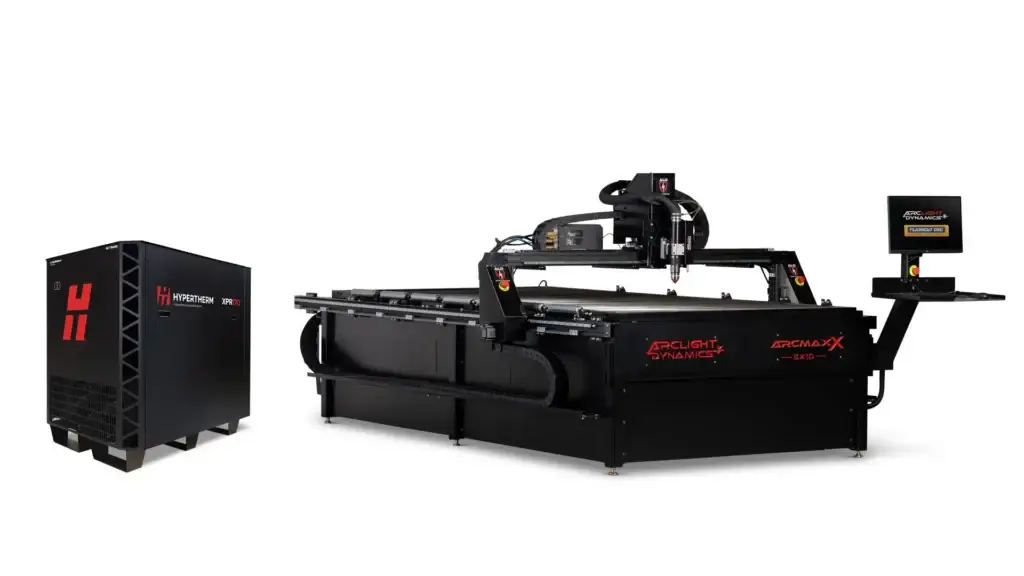
| Arc Max X | FlashCut CNC | Hypertherm XPR170 or XPR300 — included with the table | XPR170 (XPR300 for 1¾"+ pierce) | Industrial HD cutting, laser-grade edges, stainless and aluminum |
“Most common pairing” is where the majority of shops in that tier land; every table accepts the full option list, and your quote is built around the metal you actually cut.
Do You Need a Machine Torch for a CNC Plasma Table?
Yes. A CNC plasma table needs a machine torch, not the hand torch that comes in the box with most plasma cutters. A machine torch has a straight, cylindrical body that clamps squarely in the table’s torch holder, no trigger (the table fires the arc), and a lead long enough to reach the far corner of the cutting area without dragging — Arclight tables are configured with a 25-foot or 35-foot Hypertherm Duramax® machine torch lead, with the longer lead sized to the table.
The torch is also where the table’s intelligence plugs in. Arclight’s Advanced Digital Torch Height Control (DTHC), standard on every table, reads arc voltage from the cutter through the CPC port and holds the torch at the right standoff through warped plate, and the breakaway torch mount and collision detection protect the torch if it ever meets a tipped-up part. A hand torch strapped to a bracket gives you none of that. If you already own a Hypertherm Powermax with a hand torch, the fix is simple: a Hypertherm machine torch is a bolt-on swap, and Arclight stocks machine torches for every Powermax it sells, from the 45 SYNC through the 125.
What Does a CNC Plasma Table Need From the Plasma Cutter?
A CPC port and a serial interface
The CPC (machine interface) port is the connection that lets the table fire the torch, confirm the arc has transferred, and read the divided arc voltage that torch height control runs on. Every Hypertherm system Arclight sells for its tables is ordered with the CPC port, and the Powermax SYNC models add a serial (RS-485) interface so the CNC can set amperage and read cartridge data straight from the cutter — no walking to the power supply to turn the dial. If you are shopping a cutter on your own, “with CPC” is the line on the spec sheet to look for; a bare hand-held unit with no machine interface port is not a CNC cutter, no matter the amperage.
Shop power and duty cycle
The table itself is undemanding — an Arclight table runs on a standard 120 V, 15 A circuit. The plasma cutter is what sets the electrical service you need. The Powermax45 SYNC runs on single phase; the Powermax65 and 85 SYNC run on single or three phase; the Powermax105 SYNC, Powermax125, MAXPRO200 and XPR are three-phase only. If your shop is single-phase, the 85 is the practical ceiling, and it is a very capable one.
Duty cycle matters more on a CNC table than on a hand torch because the machine does not get tired. A cutter rated at 50% duty at full amperage will cut for five minutes in ten before it needs to cool; the Powermax125 and MAXPRO200 are rated at 100% duty at full amperage, with the 105 close behind, which is one more reason production shops step up even when the plate does not demand it. Air is the other requirement: plan on 15 CFM at 90 PSI from a 5 HP, 60–80 gallon compressor, and a filter and dryer — clean, dry air is the single most effective upgrade for cut quality and consumable life on any plasma system.
Consumables and cost per cut
Consumables are the real running cost of a plasma table, and amperage choice changes the math. The Powermax SYNC systems use single-piece SmartSYNC® cartridges (about $70 each on our site) that replace the five-part nozzle, electrode, swirl ring, retaining cap and shield stack, install in seconds, and tell the cutter what amperage to run. A cutter working comfortably inside its rating cuts faster and gets more starts per cartridge than one pushed to its limit — so the “bigger” system often costs less per part. The MAXPRO200 and XPR use conventional multi-piece consumable sets (starter kits run $1,130–$1,410) with far longer life at high amperage, which is where their economics win on heavy plate.
When Does HD Plasma Make Sense Over a Powermax on a CNC Table?
A Powermax is conventional air plasma: it uses shop air as both plasma and shield gas, and it delivers excellent cut quality for fabrication, signage, brackets, gussets, and structural parts. High-definition (HD) plasma — the Hypertherm XPR family on the Arc Max X — uses a constricted, higher-energy arc with oxygen, nitrogen, or argon-hydrogen mixes chosen per material, and it changes what plasma can do: near-square edges, minimal dross, bolt-ready holes, and consistent quality from 26-gauge to 1¾" pierce. HD is the right call when you are competing with laser shops on edge quality, when your parts go straight to weld fixtures with no grinding, or when you cut a lot of stainless and aluminum and need clean, oxide-free edges.
| Conventional air plasma (Powermax SYNC, MAXPRO200) | High-definition plasma (XPR170 / XPR300) | |
|---|---|---|
| Arclight tables | Arc Pro Ultra V3, Arc Pro Elite V3, Arc Max Ultra, Arc Max Elite, Arc Max Unlimited | Arc Max X 5×10 and 6×12 |
| Gases | Shop air (nitrogen optional on some Powermax models) | O₂, N₂, air, argon-H₂ and mixes, selected per material by the gas console |
| Edge quality | Good to very good; light bevel and some dross on thick plate | Near-square, minimal dross, oxide-free on stainless and aluminum with the right gas |
| Holes | Usable; smaller holes need cleanup | Bolt-ready holes with far less taper |
| Pierce range (mild steel) | ½" to 1¼" depending on amperage | 1⅜" (XPR170) to 1¾"–2" (XPR300) |
| Power | Single phase up to the 85; three phase above | Three phase |
| What it costs | $3,710–$22,245 added to a table quote | Included: Arc Max X runs $160,995–$182,995 complete with XPR, Core Plus gas console, 3-day onsite install and training |
Most shops are well served by conventional plasma. HD plasma is a throughput and finish decision, not a thickness decision — a MAXPRO200 on an Arc Max Unlimited pierces thicker plate than an XPR170.
Can You Use Your Own Plasma Cutter on a CNC Table?
Sometimes — and the honest answer depends on what you own. To work on a CNC table a plasma cutter needs a machine torch, a CPC machine-interface port with a voltage-divider output for torch height control, and enough amperage and duty cycle for the plate you cut. A Hypertherm Powermax with CPC checks every box, and if yours has a hand torch the machine torch is a bolt-on swap. A budget cutter with no machine interface, a high-frequency start that interferes with electronics, or a fixed hand torch is a poor fit for a CNC table regardless of price.
On the Arc Max Unlimited, the configurator includes a “provide your own plasma cutter” option for shops that already run a compatible system. On the Arc Pro lines, the entry option is a Razor Cut 45di (torch included), and every table can be quoted with a Powermax45 SYNC as the lowest-cost Hypertherm path. Not sure what you have? Tell us the model and we will tell you whether it belongs on the table or in the truck as your portable cutter — a lot of owners keep both.
Plasma Cutters for CNC Tables: Frequently Asked Questions
What size plasma cutter do I need for a CNC table?
Size it to the thickest metal you cut every day. A Hypertherm Powermax45 SYNC pierces ½" mild steel, the Powermax65 pierces ⅝", the Powermax85 pierces ¾", the Powermax105 pierces ⅞", and the Powermax125 pierces 1". If you nest parts out of ½" plate all day, step up to a 65 or 85 for speed and consumable life rather than running a 45 at its limit.
Do I need a machine torch for a CNC plasma table?
Yes. A machine torch has a straight body that clamps squarely in the table’s torch holder, no trigger, and a 25- or 35-foot lead to reach the whole cutting area. It also carries the connections torch height control depends on. A hand torch can be strapped to a bracket, but you lose accurate height control and torch protection. Hypertherm machine torches are available for every Powermax from the 45 SYNC through the 125.
Should I get a Powermax45 or a Powermax65 for 1/2-inch steel?
Both will do it, but for different jobs. The Powermax45 SYNC is rated to pierce ½" and is the right choice if ½" is your occasional maximum. If ½" is your everyday material, the Powermax65 SYNC pierces it faster, cuts it cleaner, gets more starts per consumable set, and leaves headroom to ⅝". For a single-phase shop that cuts plate daily, the Powermax85 SYNC is the practical ceiling and the most common production pick.
What is the difference between conventional and HD plasma?
Conventional air plasma (Hypertherm Powermax and MAXPRO200) uses shop air and delivers excellent fabrication-grade cuts. High-definition plasma (Hypertherm XPR170 and XPR300 on the Arc Max X) uses a constricted, higher-energy arc with oxygen, nitrogen, or argon-hydrogen gases selected per material, producing near-square edges, minimal dross, and bolt-ready holes. HD is a finish and throughput upgrade; the MAXPRO200 still pierces thicker plate than an XPR170.
Does the plasma cutter come with an Arclight table?
The plasma cutter is configured with your quote so it matches the thickness and volume you cut — you choose it as the first line of every Arclight table’s configurator, from a Powermax45 SYNC through a MAXPRO200. The exception is the Arc Max X, which is sold as a complete system with the Hypertherm XPR170 or XPR300, the gas console, and onsite installation and training included.
Can I use my existing plasma cutter on a CNC table?
If it is a Hypertherm Powermax with a CPC machine-interface port, yes — add a Duramax machine torch if it came with a hand torch. Other cutters need the same things: a machine torch, a CPC port with a voltage-divider output for torch height control, and adequate amperage and duty cycle. The Arc Max Unlimited configurator includes a provide-your-own-cutter option; for any other table, send Arclight the model and we will tell you whether it is a fit.
Keep Researching
- Choosing a CNC Plasma Table: The Complete Buyer’s Guide — size, shop space, thickness, controllers, air and power, spec by spec
- What Is the Best CNC Plasma Table for a Small Shop? — which table, which cutter, and what it costs together
- How Much Does a CNC Plasma Table Cost? — 2026 prices for every Arclight series and what else to budget for
- CNC Plasma Cutting Tips — get the most out of whichever cutter you choose
- Hypertherm plasma cutters — the Powermax SYNC, Powermax125 and MAXPRO200 systems Arclight sells and supports
- Arc Max X HD CNC plasma table — the Hypertherm XPR170 / XPR300 system
Get the Right Cutter Quoted With Your Table
Tell us what you cut — material, thickness, and how many hours a week — and we’ll quote the table, size, and Hypertherm system for the job. Transparent pricing, no hidden line items.
$500 locks in your price and your build slot · 30-day satisfaction guarantee · Lifetime tech support that follows the table